Improve 3D Print Quality: 6 Common Problems and How to Fix Them
Sep 26, 2026

Are you constantly struggling with uneven printed layers? Is your printer leaving huge blobs and unwanted stringy plastic threads?
If the answer is yes, you have come to the right place. 3D print quality can be managed with some quick and easy remedies: often the cause is a small technical error that even experts miss. This is your guide to improving the print quality of your end products.
We will look at design changes that improve print quality, then at the six problems every 3D printer runs into:
- Stringing
- Layer shifting
- Blobs on the surface
- Ringing (ghosting)
- Sagging or drooping
- Warping
Things to keep in mind during the design phase
It is important to understand the features of the printer you are using. Three key aspects account for making sensible adjustments in the settings: precision, accuracy and tolerance.
Even before you jump into production, there are quality checks you can carry out as a precaution to avoid obvious mistakes.
1. Keep a note of the surface quality
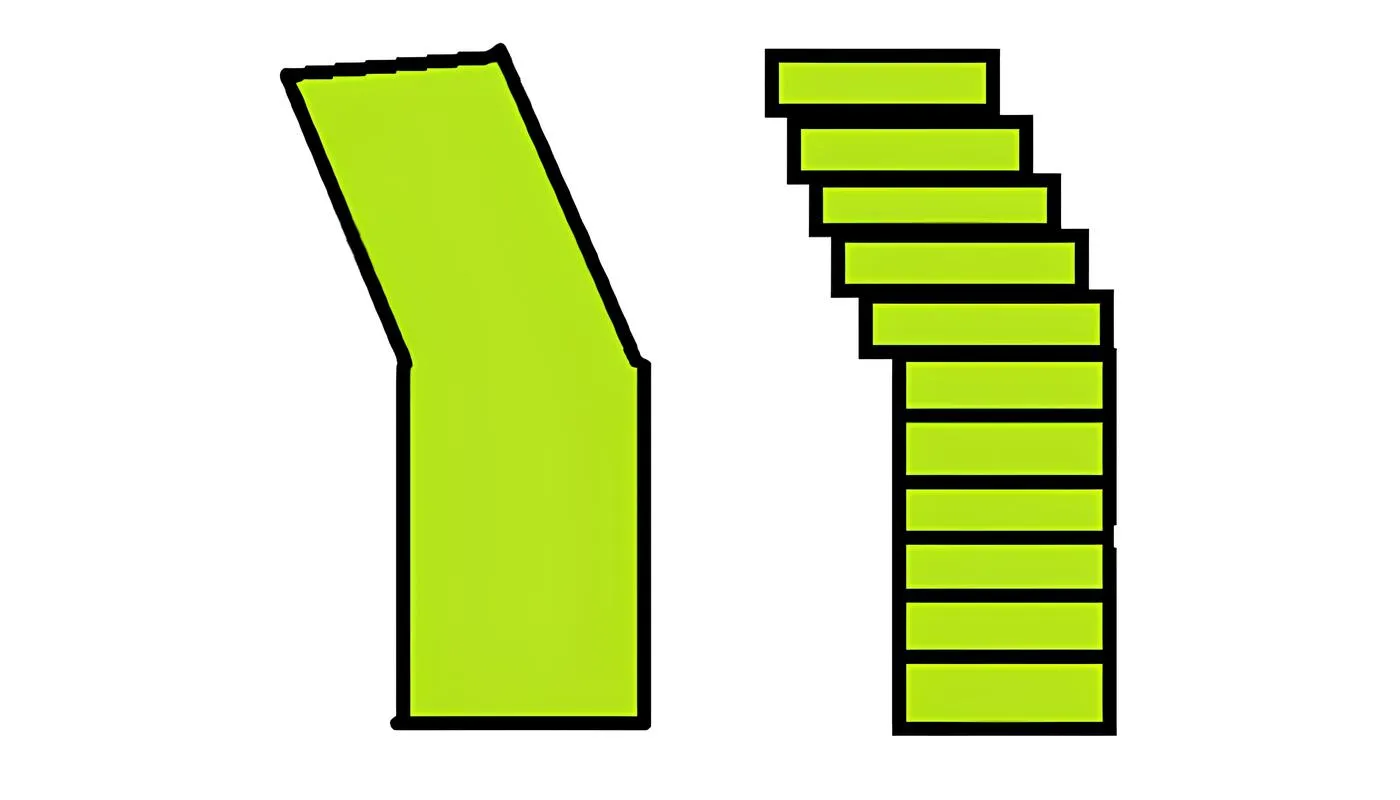
Avoid using inclined planes if you want a shiny object. There is a phenomenon called the staircase effect that makes surfaces look rough and edgy. Stick to horizontal or vertical planes.
2. Minimise shrinkage
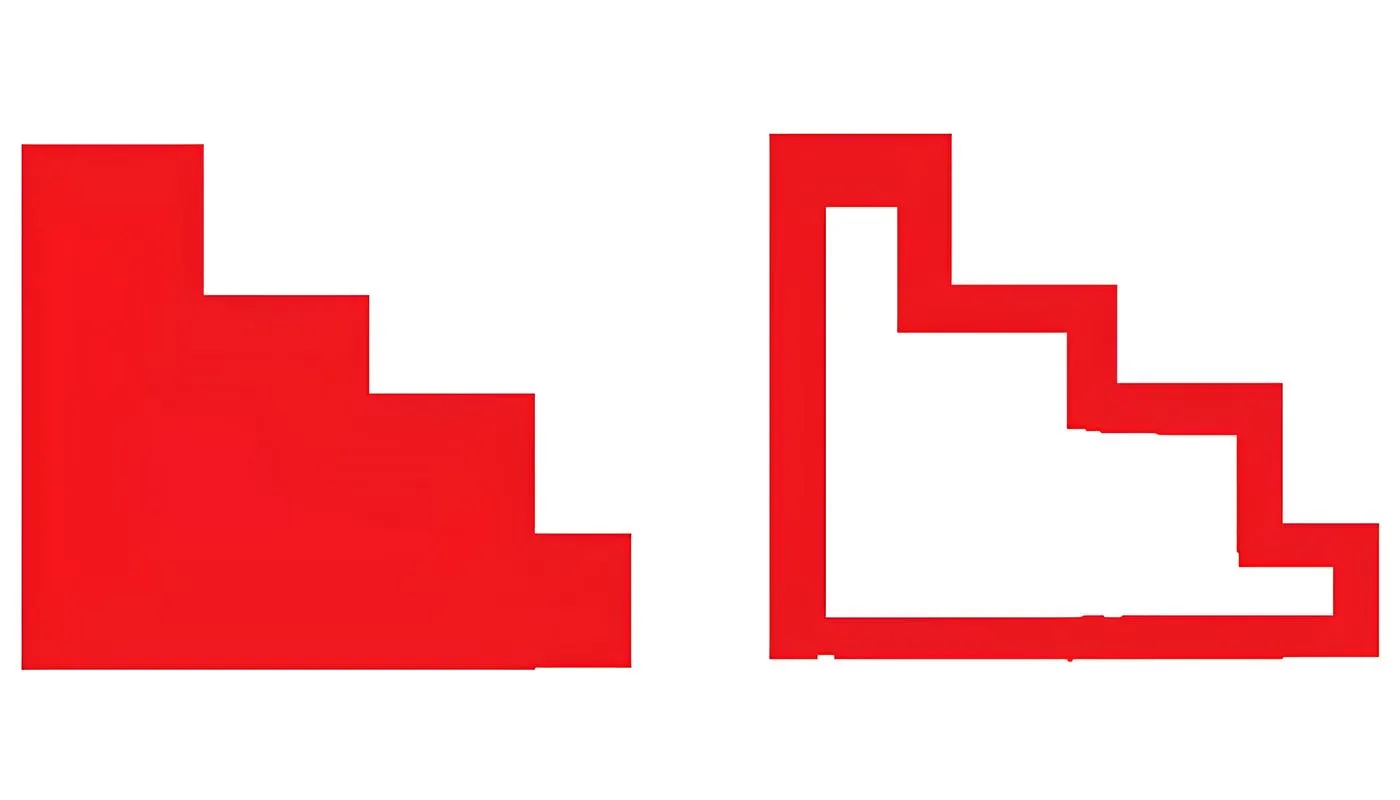
Shrinking and expansion of material occur during the printing and cooling phases, and shrinkage can take a part out of tolerance. How much depends on the material: ABS is more susceptible than PLA. One way to deal with it is to use uniform wall thickness, which prevents large chunks of material from coming together and lets it spread evenly on heating. In the picture below, the design on the right is the better alternative, as there is enough room for expansion.
3. Use minimal support structures
Overhanging parts of a model need support structures. These are usually needed for:
- Any surface at an angle of less than 45 degrees to the print plane
- Long horizontal structures like a bridge
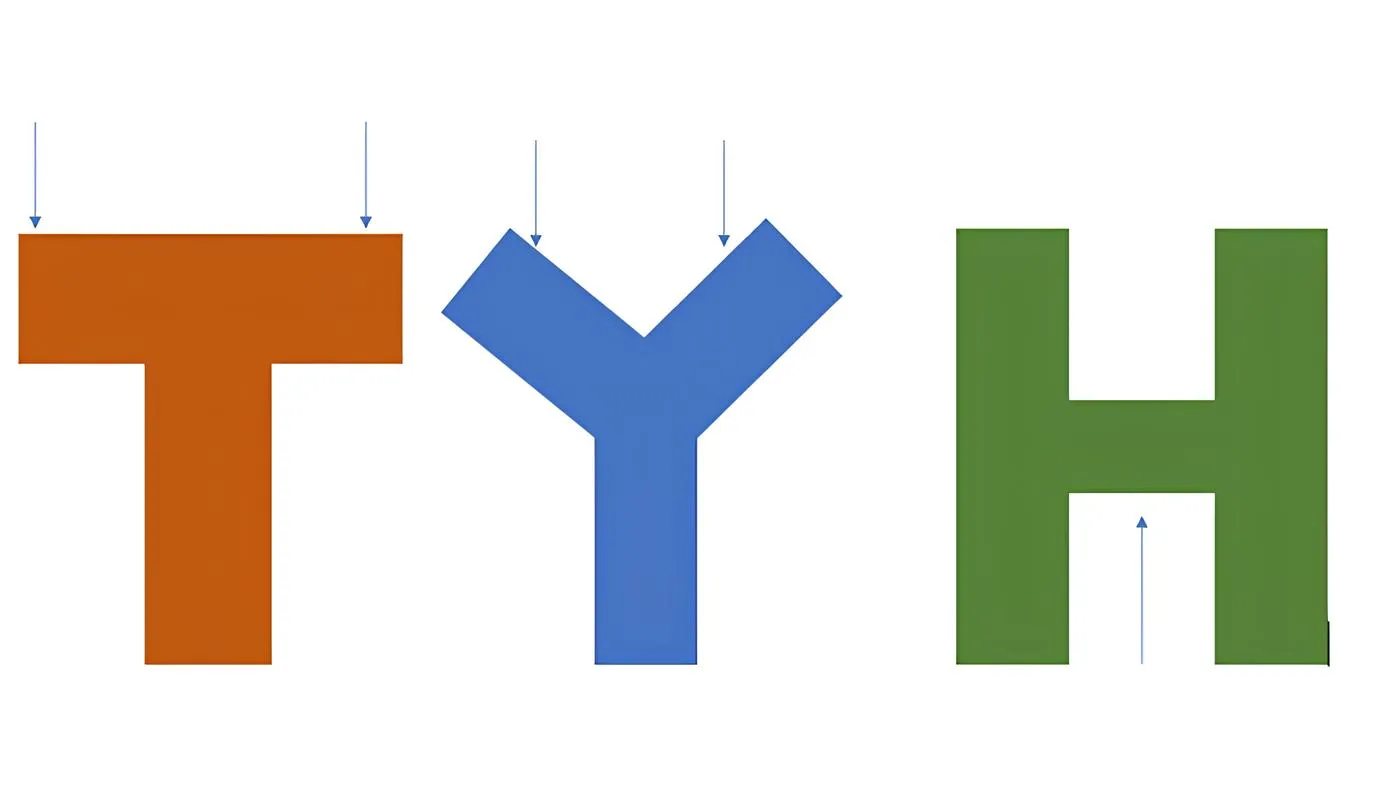
It helps to minimise supports by modifying the design itself. Take the letters T and Y: the Y can be printed without supports because of the angles on its arms, while the T has an angle to the horizontal of less than 45 degrees, so supports are required.
The design and planning phase is where you prevent the errors that most affect final print quality. Do not be afraid to experiment with different settings: it will help you understand what each one does to the end product.
Quick fixes for 3D print quality issues
1. 3D print stringing: why it happens and how to fix it
In short: stringing happens because plastic oozes from the nozzle while the extruder travels between points. The fix is retraction: pulling filament back before each move, plus a small drop in nozzle temperature.
The problem
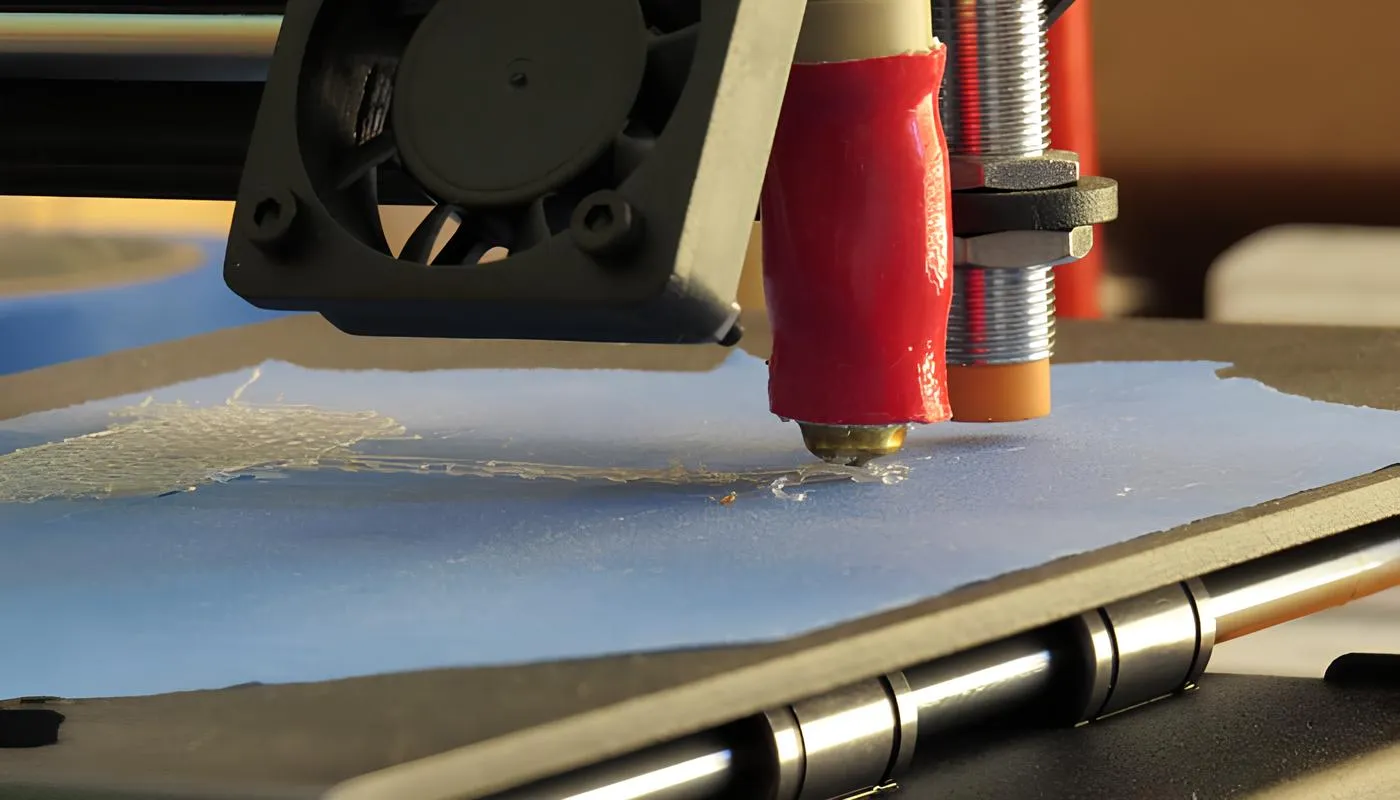
The finished model has strands of plastic left behind, sometimes called 'hairy' prints. The cause lies in the way the extruder moves: every time it travels to a new location, plastic oozes from the nozzle and leaves an unwanted strand. This can be fixed with a setting almost every 3D printer has: retraction.
The solution
Start with the retraction settings. Retraction distance controls how much plastic is pulled back from the nozzle, to prevent oozing while the head moves to a new spot. Different extruders need different distances: Bowden extruders need around 15 mm, while direct drive extruders need roughly 0.2–0.5 mm.
Another cause of oozing is excessive melting at high temperature, which lets plastic leak from the nozzle. Adjust the temperature down by 2–5 degrees and see whether the stringing stops. Also make sure your printer has a cooling fan close to the nozzle.
Play with the settings to find the right fit for your prints. Stringing happens on long travel moves, so adjusting the X-Y axis settings is where to look.
2. Layer shifting in 3D prints: causes and fixes
In short: layers shift because the print head loses position and the printer has no feedback to detect it. Reduce print speed and acceleration, check belt tension, and make sure the power supply is stable.
The problem
To get precise dimensions, the tool head needs to move to the correct place and print the layer. Unless you are using costly embedded control systems, there is no mechanism for the printer to check whether that location is accurate (no feedback loop). So if the printer is knocked mid-process and the tool head is displaced, the layers shift and the structure deforms.
The solution
The most direct fix is print speed. Default settings can be changed to a speed that prevents shifting, and the X-Y movement speed should be reduced to whatever suits your design. Decreasing acceleration and jerk values in the firmware also reduces the chance of a shift. At Fabheads we provide calibrated motion settings for each tool head used with our fabmachines printers.
If layers still form unevenly after adjusting speed, look at belt tension. Belt tension drives the pulley action of the printer, and if it is too loose or too tight it will cause problems.
Another cause is a fluctuating power source, which produces erratic motor movement. Make sure the supply is stable by using a UPS or fitting suitable noise filters.
3. Blobs on 3D prints: how to remove them
In short: blobs form where the extruder stops and restarts on the same spot. Adjust retraction for blobs at the start of a print, and enable coasting for blobs at the end.
The problem
Blobs on the flat surfaces of a model are a common complaint. They occur when the extruder is interrupted or has to restart printing from the same spot, depositing material on top of what is already there. They are very hard to cut off after printing and cooling.
The solution
Like stringing, this is a retraction issue, but first identify whether the blobs appear at the start or the end of the print.
- At the start: adjust the retraction setting so the extruder knows exactly where printing should resume.
- At the end: use coasting, which stops extrusion a set moment before the end of the move.
4. 3D printer ringing (ghosting): what causes it
In short: ringing is a vibration artefact caused by sudden direction changes at speed. Reduce acceleration in firmware, lower X-Y speed, and make sure the printer frame and table are rigid.
The problem
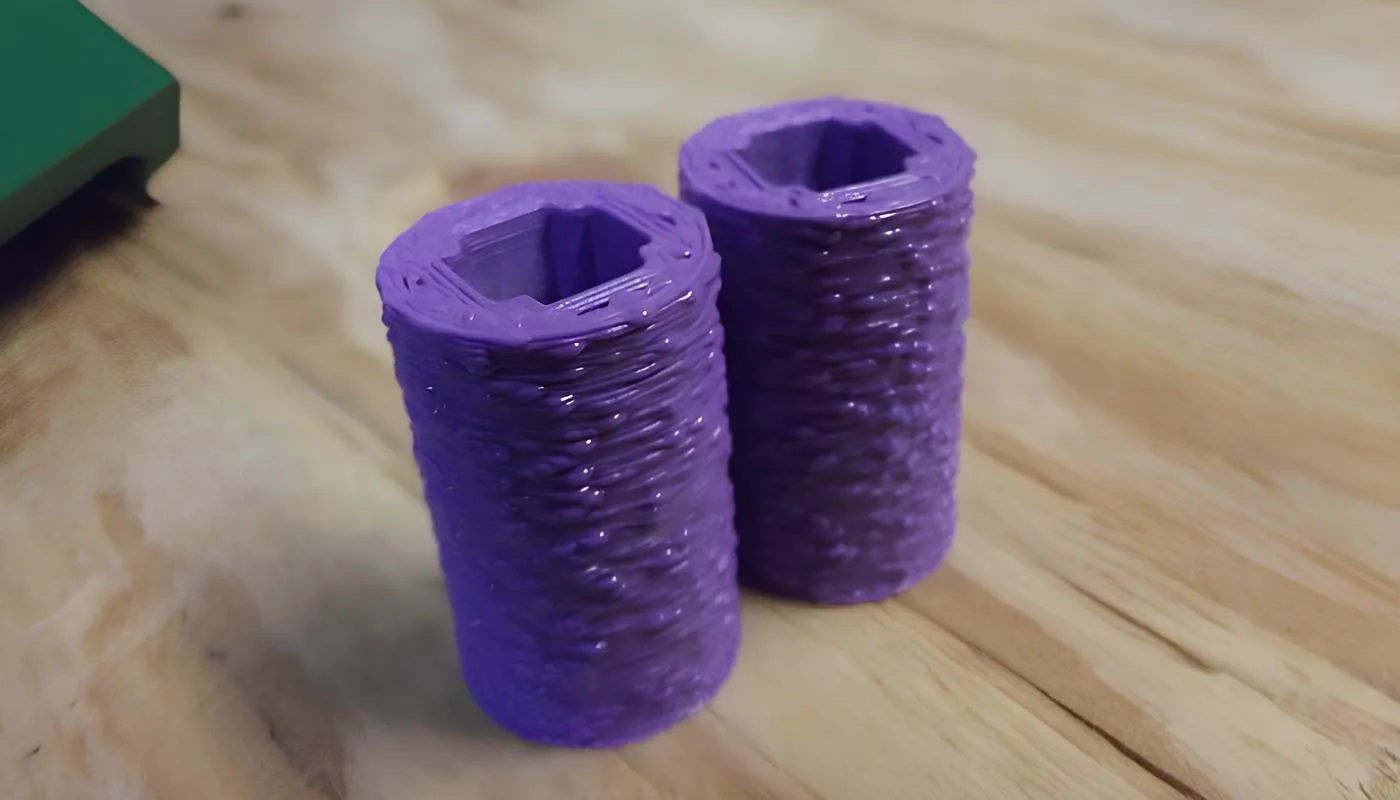
Unwanted ripple patterns appear on surfaces, usually at edges or corners. The sudden change of direction for the extruder causes vibration. On flat, even, geometric objects it looks poor.
The solution
There are three causes, and each has a fix:
- Firmware acceleration. The firmware controls the acceleration of the tool head. Reducing it by a few notches often prevents ringing outright.
- Printer speed. As with layer shifting, the X-Y axis speed needs adjusting.
- Mechanical looseness. Check the surface board placement, make sure the table the printer sits on is not shaky, and confirm the frame is rigid and the fasteners have not loosened through continuous use.
5. Sagging and drooping in bridges
In short: unsupported spans droop as they cool. Enable your slicer's bridging settings, check the infill direction, and add supports if the span is long.
The problem
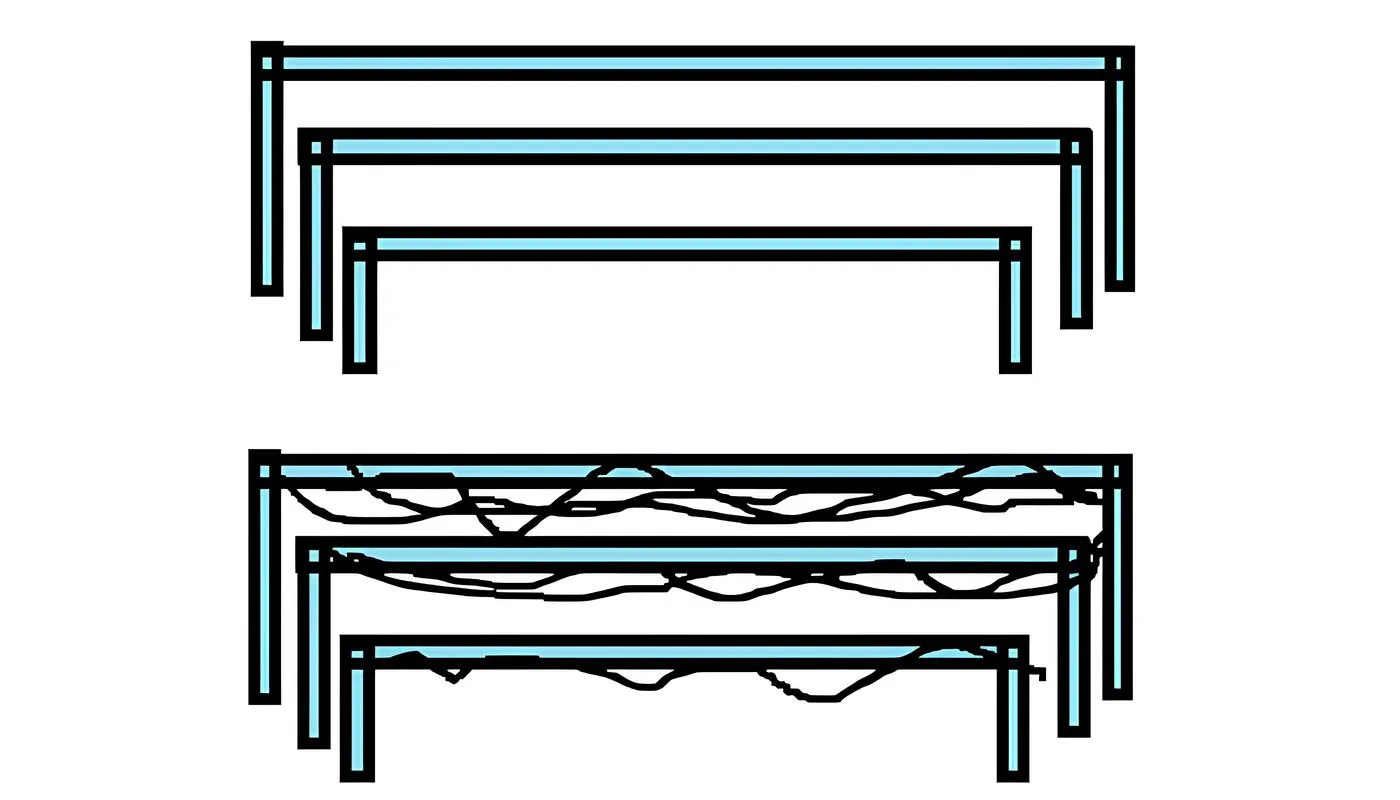
When a block of plastic has no support in the middle, the middle portion tends to droop slightly after rapid cooling. The lack of support causes the sagging, and it is most prominent in long bridge-like structures.
The solution
Infill direction plays a large role in printing bridge structures. Check that the axis selected in the slicer is correct: most printers handle infill direction automatically.
Next, check the bridging settings. These highlight the bridge section, after which the printer manages the portions that might sag, using specific cooling temperature and speed values for those moves. If problems persist on a long span, add supporting clips to balance the model.
6. 3D print warping: how to prevent it
In short: warping happens when lower layers cool faster than upper ones and contract. Use a heated bed at around 100–120°C, run a part cooling fan near the nozzle, and print in an enclosed chamber.
The problem
You print a model you are pleased with, then notice the ends curling up, or the whole part shrinking and looking thin. That is warping. Materials such as ABS need high-temperature zones and have a long cooling time, during which internal structural changes occur.
The solution
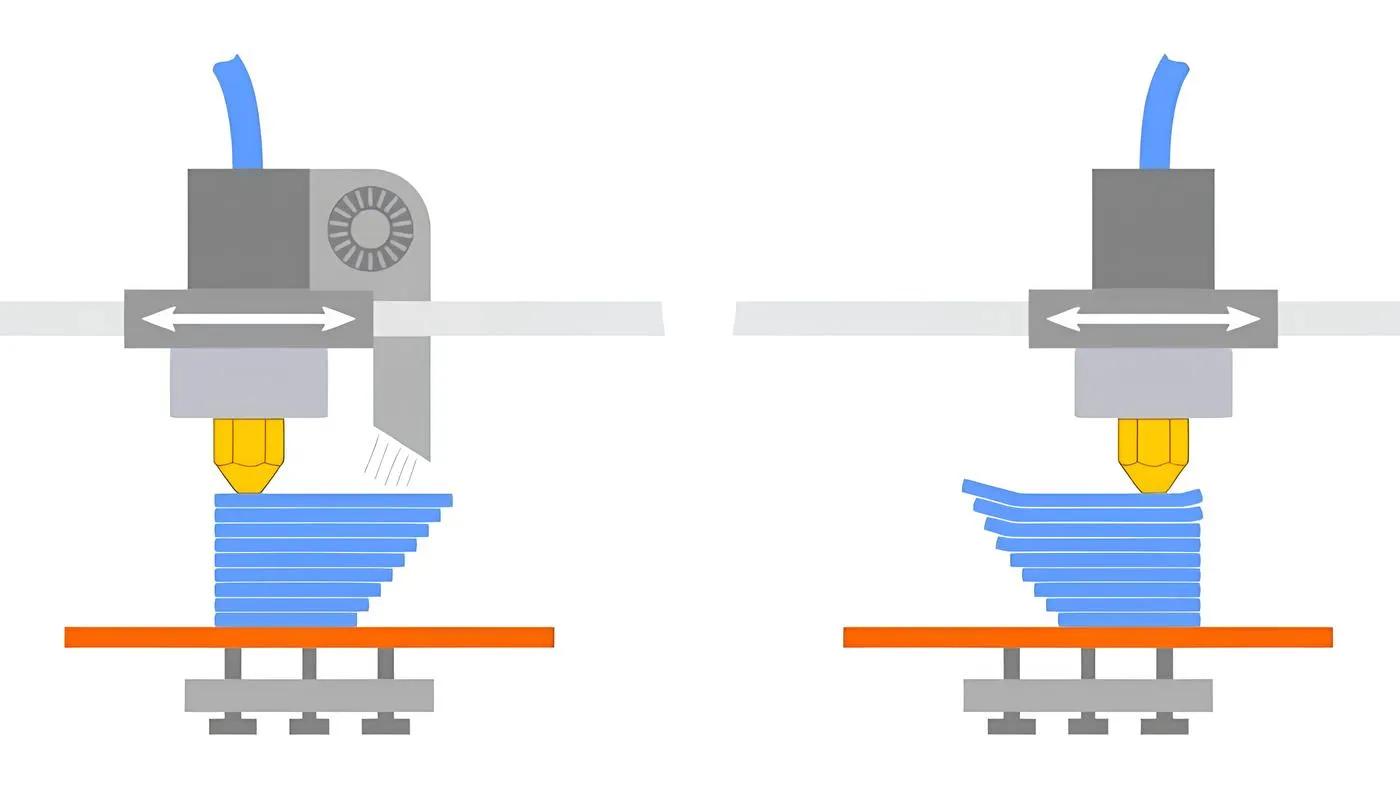
Warping occurs when the top layers are printed while the bottom layers cool too soon. A heated bed, kept hot for the entire print, addresses this: an optimal temperature is around 100–120°C. A cooling fan near the nozzle helps the top layers cool a little faster, so the bottom layers are not affected as harshly. It is also worth moving the printer from an open environment into a closed chamber, which helps with insulation and temperature regulation.
Print quality can be managed through the overall setup of your printer, the software settings, maintaining optimal temperatures, or using better equipment (nozzles, extruders and so on). Small tweaks go a long way. Where a printed plastic part simply will not meet the requirement, the answer is usually the material rather than the settings, which is where continuous fiber printing comes in.
Conclusion
Here is a quick run-through of everything covered:
- Plan the design of your product to avoid problems while printing
- Focus on simple design alterations to avoid major mishaps
- Adjust the settings that cause stringing, layer shifting, blobs, ringing, sagging and warping
- Always run a sample before committing to the final design
We hope this helps you improve the print quality of your products. If you are producing parts where quality has to be repeatable at production scale rather than print by print, our composite manufacturing services cover aerospace, mobility, marine and robotics.
Need parts where print quality has to be production-grade every time? Talk to our team.
Frequently Asked Questions
How do I stop 3D print stringing?
Increase retraction distance so filament is pulled back before travel moves: around 15 mm for Bowden extruders, 0.2–0.5 mm for direct drive. If stringing persists, lower nozzle temperature by 2–5 degrees and check that a cooling fan sits near the nozzle.
What causes ringing or ghosting on 3D prints?
Vibration from sudden changes of direction at speed. Reduce acceleration in the printer firmware, lower the X-Y axis speed, and check that the frame is rigid, the fasteners are tight and the table is not shaky.
Why do my 3D prints warp?
Because the bottom layers cool and contract while the upper layers are still being printed. Use a heated bed at around 100–120°C for the full print, run a part cooling fan near the nozzle, and print in an enclosed chamber. ABS warps more readily than PLA.
What causes layer shifting in 3D printing?
The print head losing position mid-print, with no feedback system to detect it. Reduce print speed, acceleration and jerk values; check belt tension is neither loose nor over-tight; and make sure the power supply is stable.
How do I get rid of blobs on 3D prints?
Identify whether they appear at the start or end of a print. Blobs at the start are a retraction problem: adjust the retraction setting. Blobs at the end are fixed with coasting, which stops extrusion shortly before the move completes.